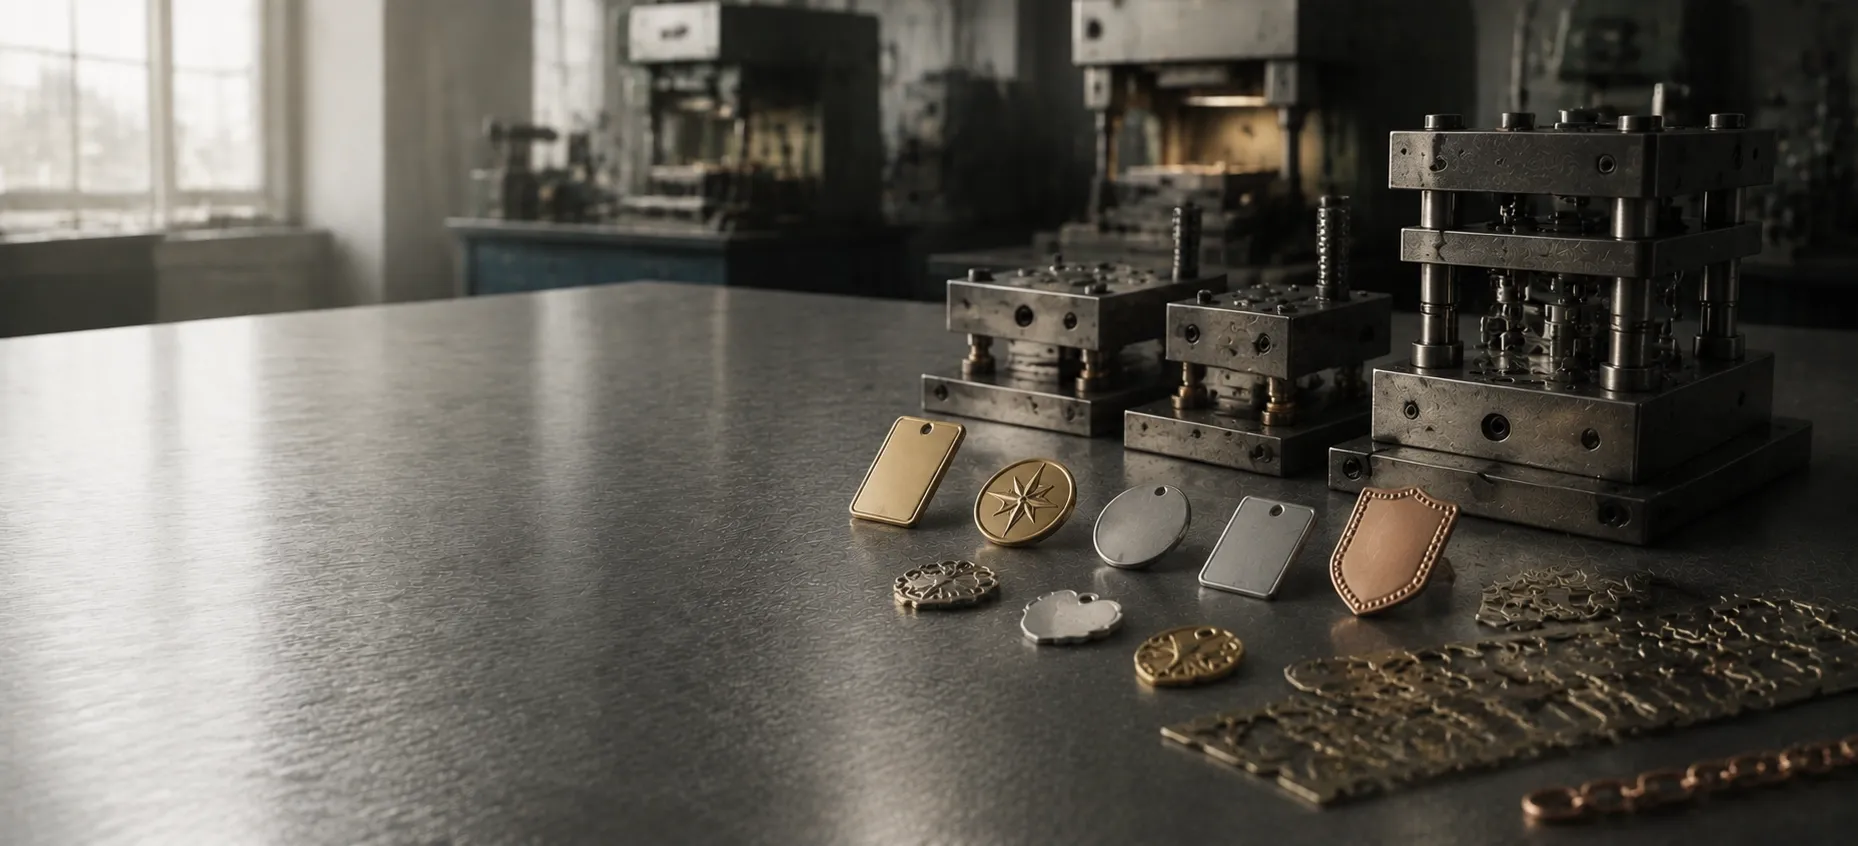
Stamping and die striking
Sheet or coil stock is blanked, formed and embossed between a matched pair of hardened steel dies under press tonnage.
- Tolerance
- ±0.05 mm
- Min. wall
- 0.3 mm
- Tooling
- $150–2,000 (simple to progressive steel die)
- Batch fit
- 1,000–500,000 pcs
How it works
Sheet or coil stock is blanked, formed and embossed between a matched pair of hardened steel dies under press tonnage.
Tags, discs, coin pendants, flat signet faces, blanks for further forming are the work this route is chosen for. It runs on 316L stainless steel, Brass, Copper, Titanium and suits 1,000–500,000 pcs.
Production steps
Each step below is a separate labour operation, and labour is priced per operation rather than per piece. That is why a 6-step route costs what it does.
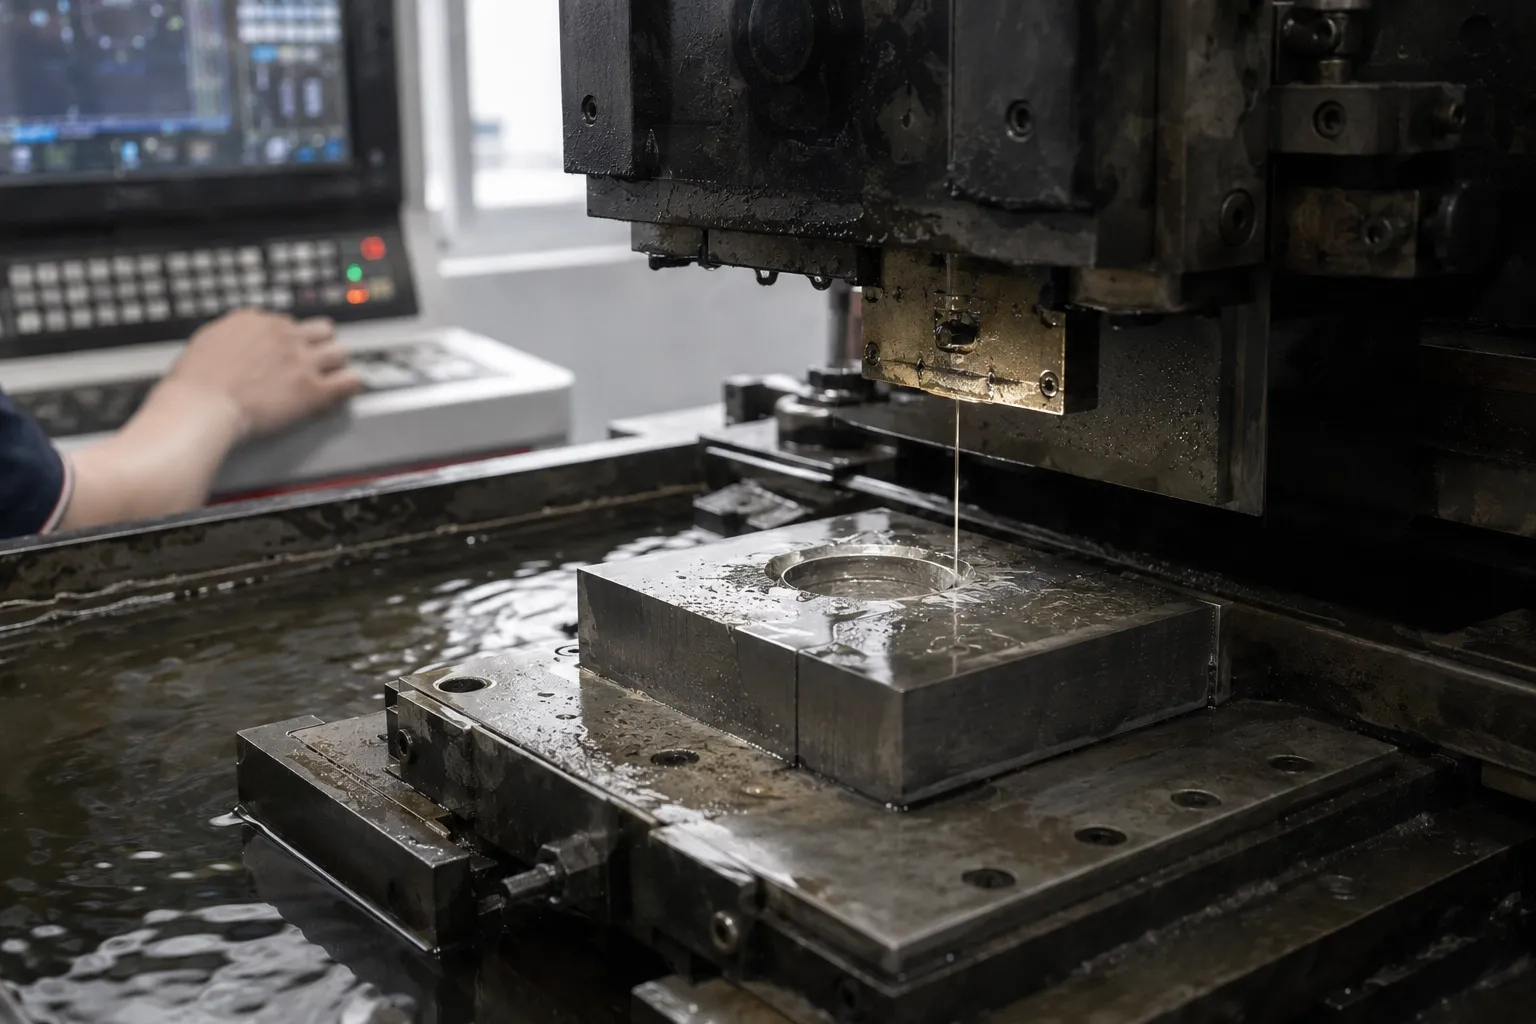
Die designed from the CAD file and cut on wire EDM 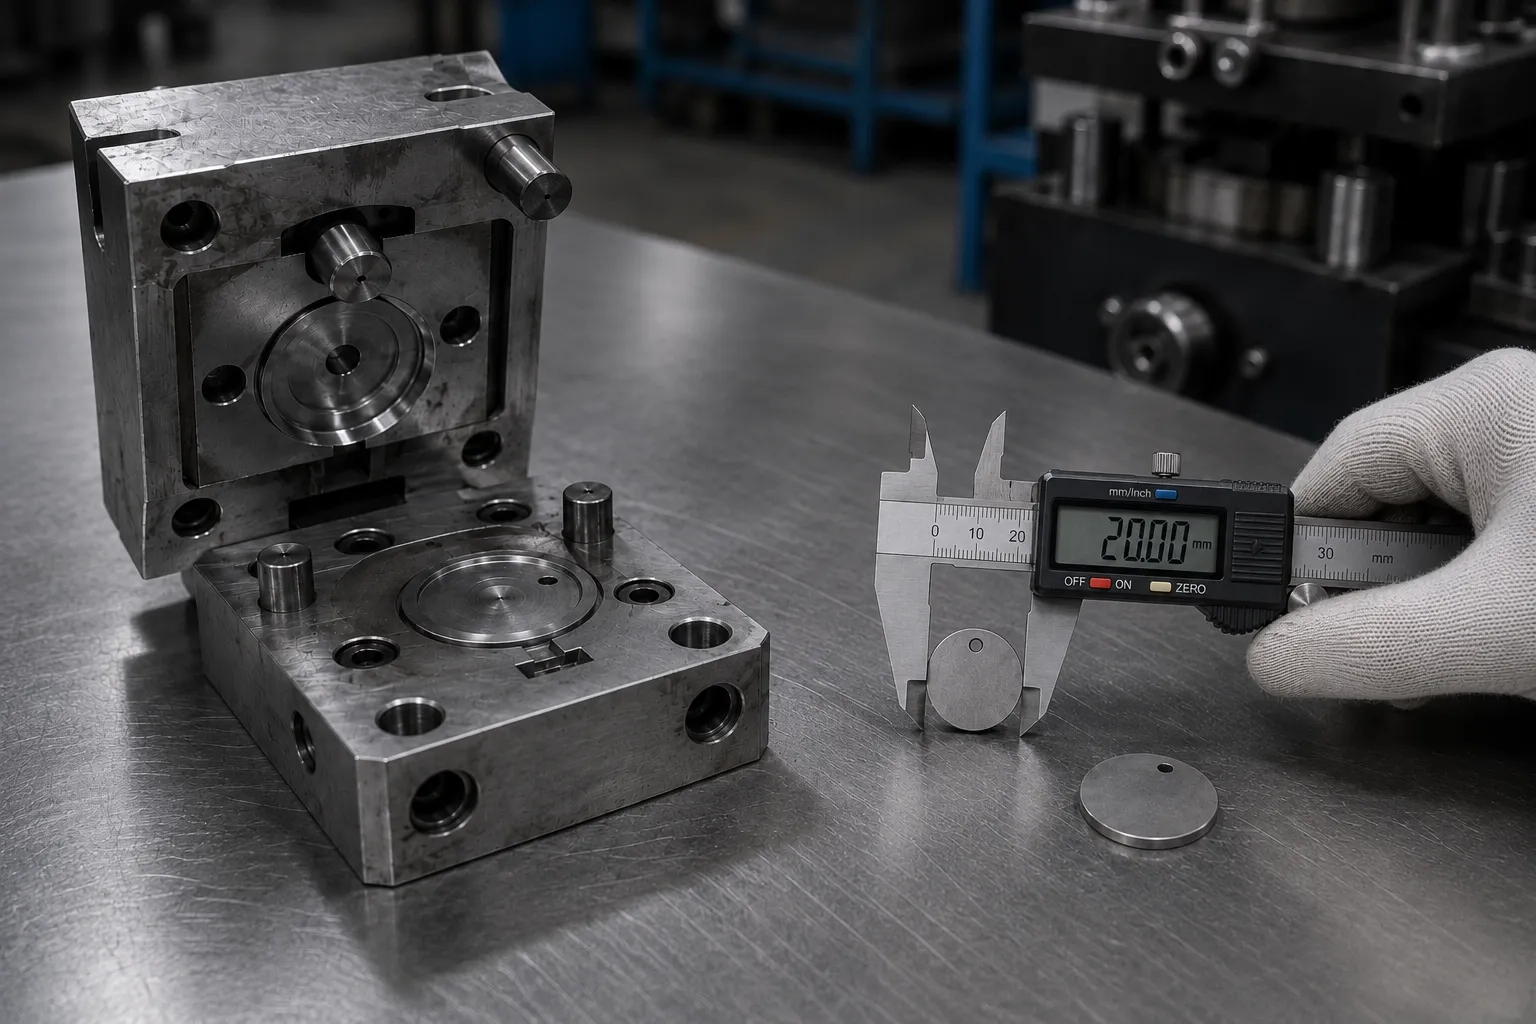
Die trialled and adjusted against a first article 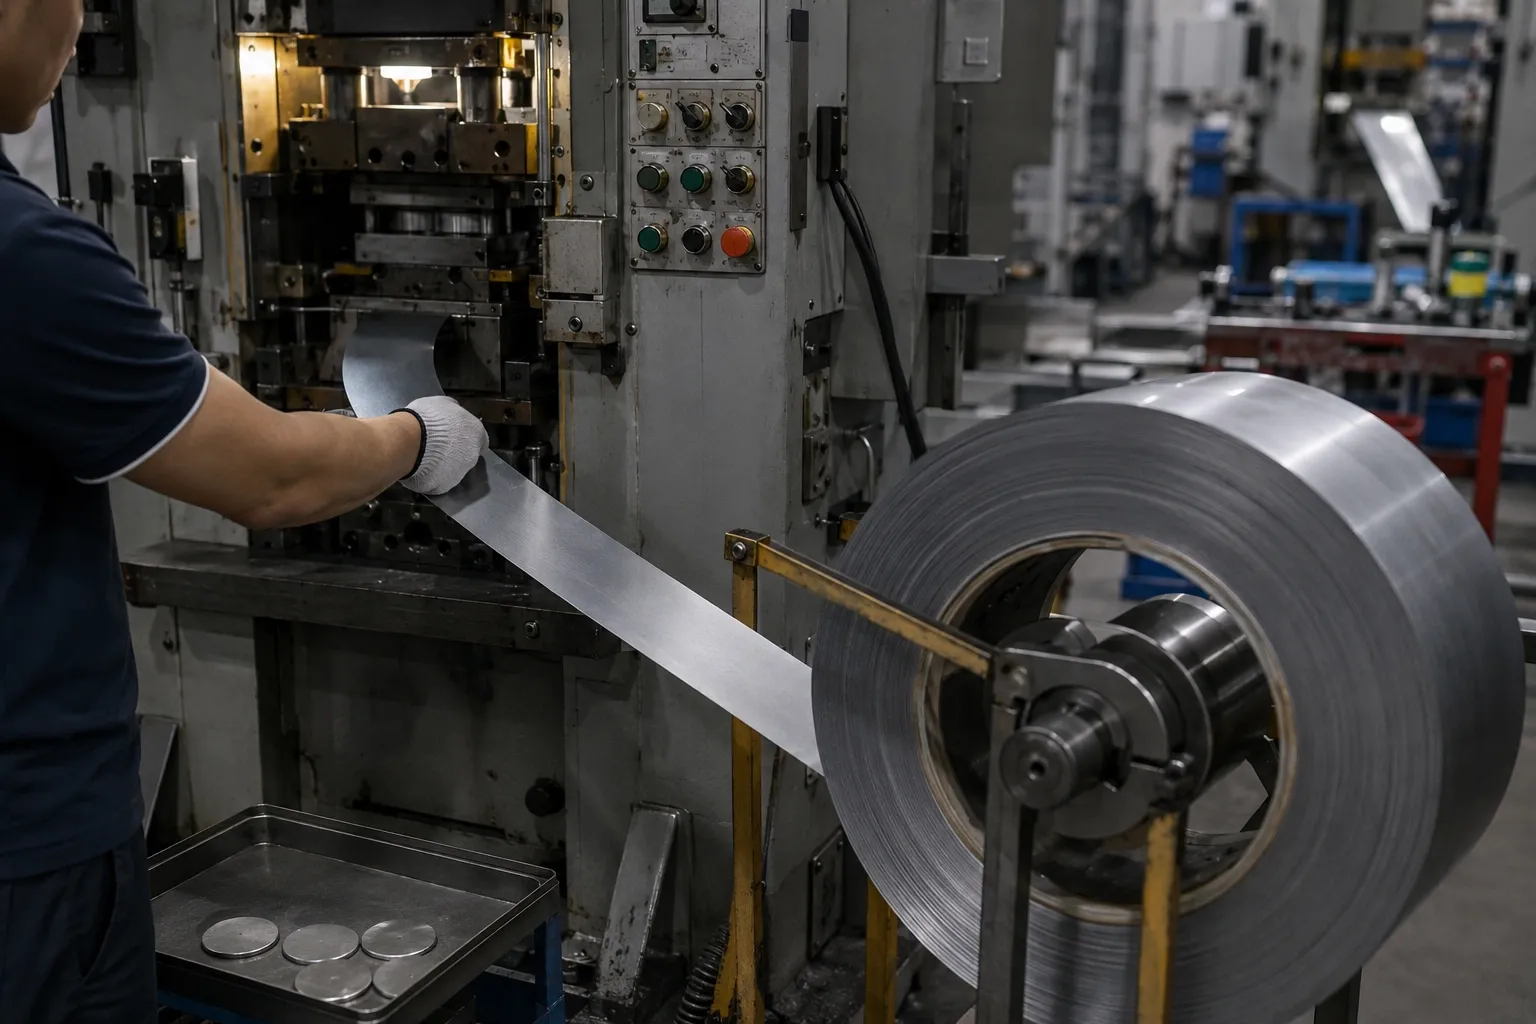
Coil or sheet stock fed into the press 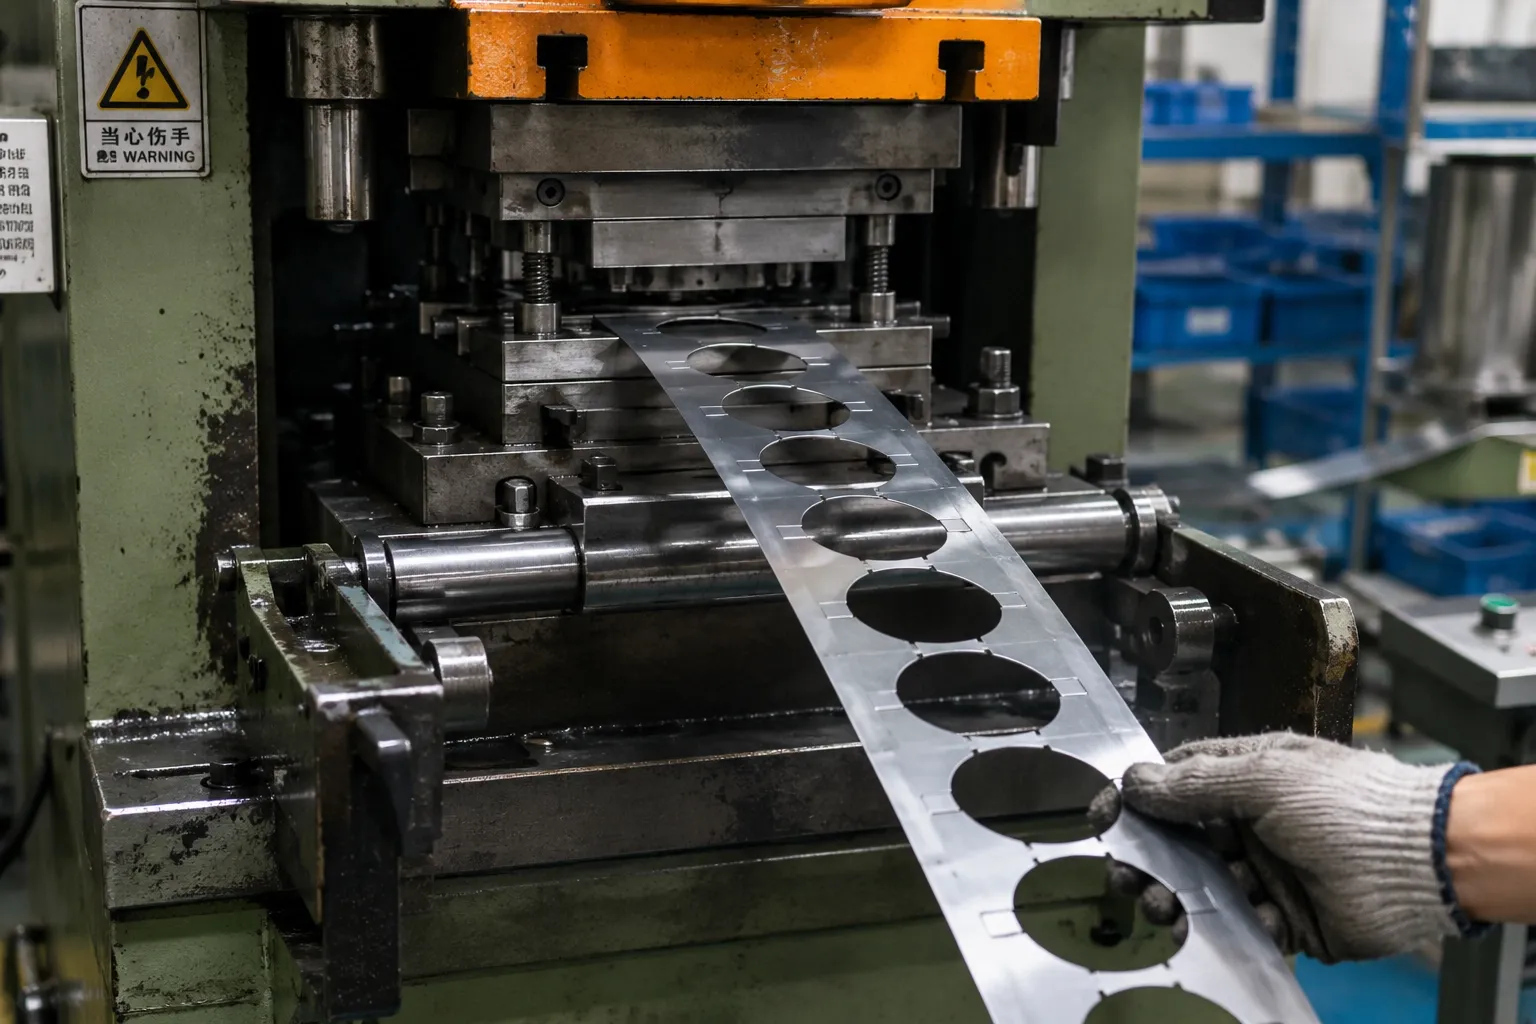
Blanking, forming and embossing — one stroke per station 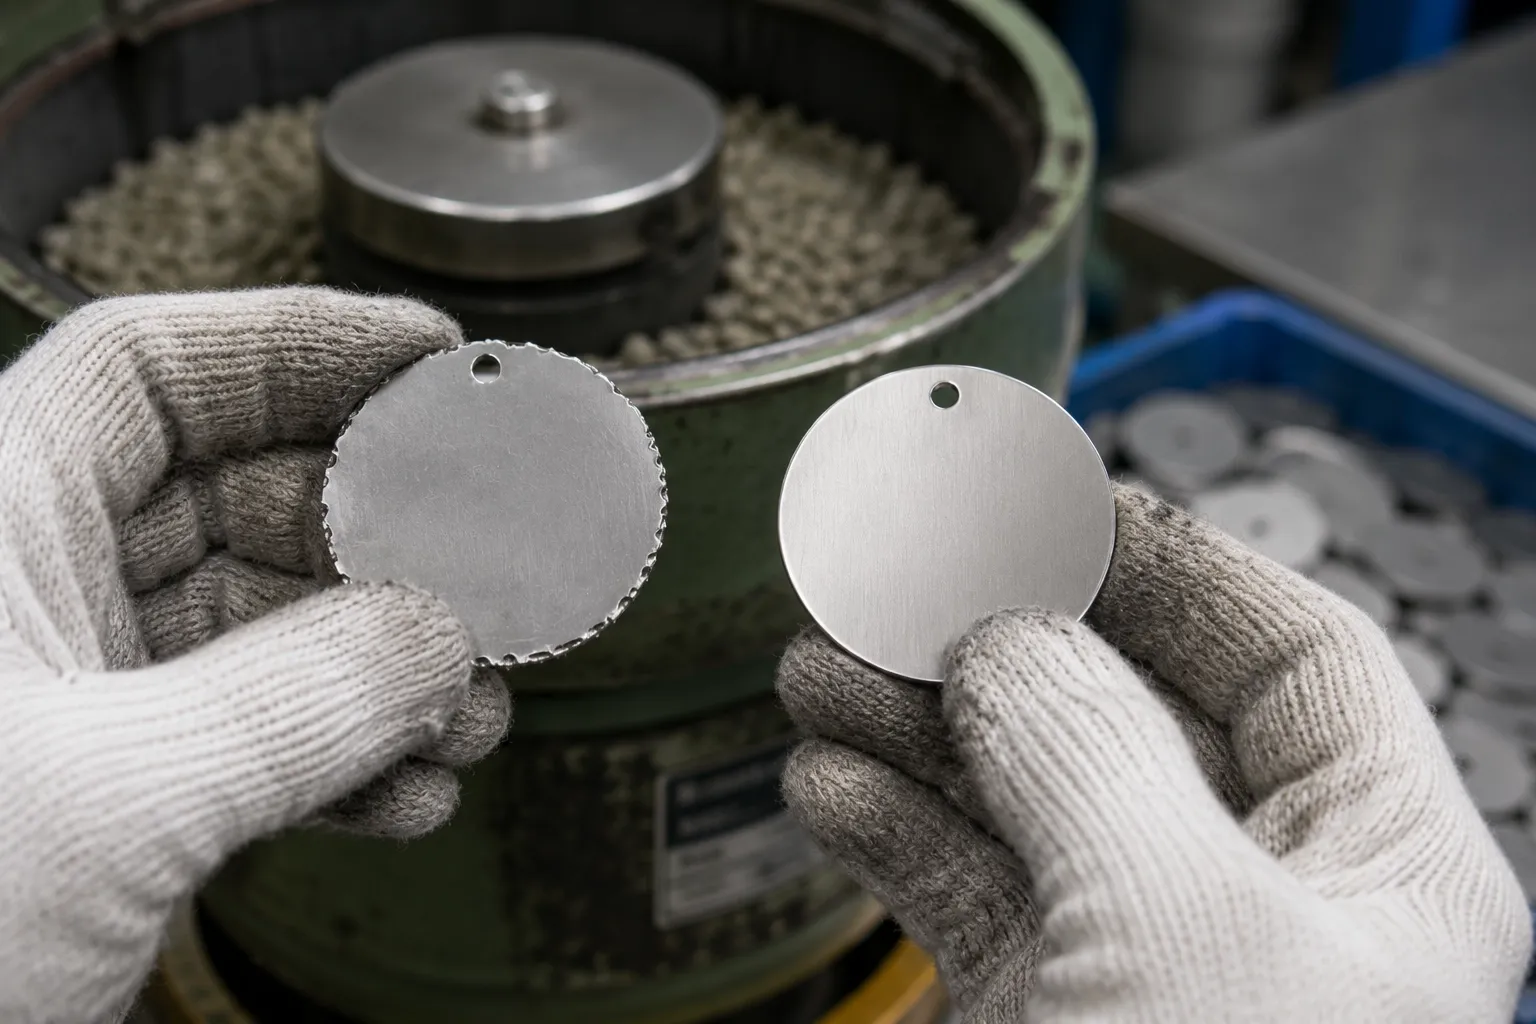
Deburring and edge finishing 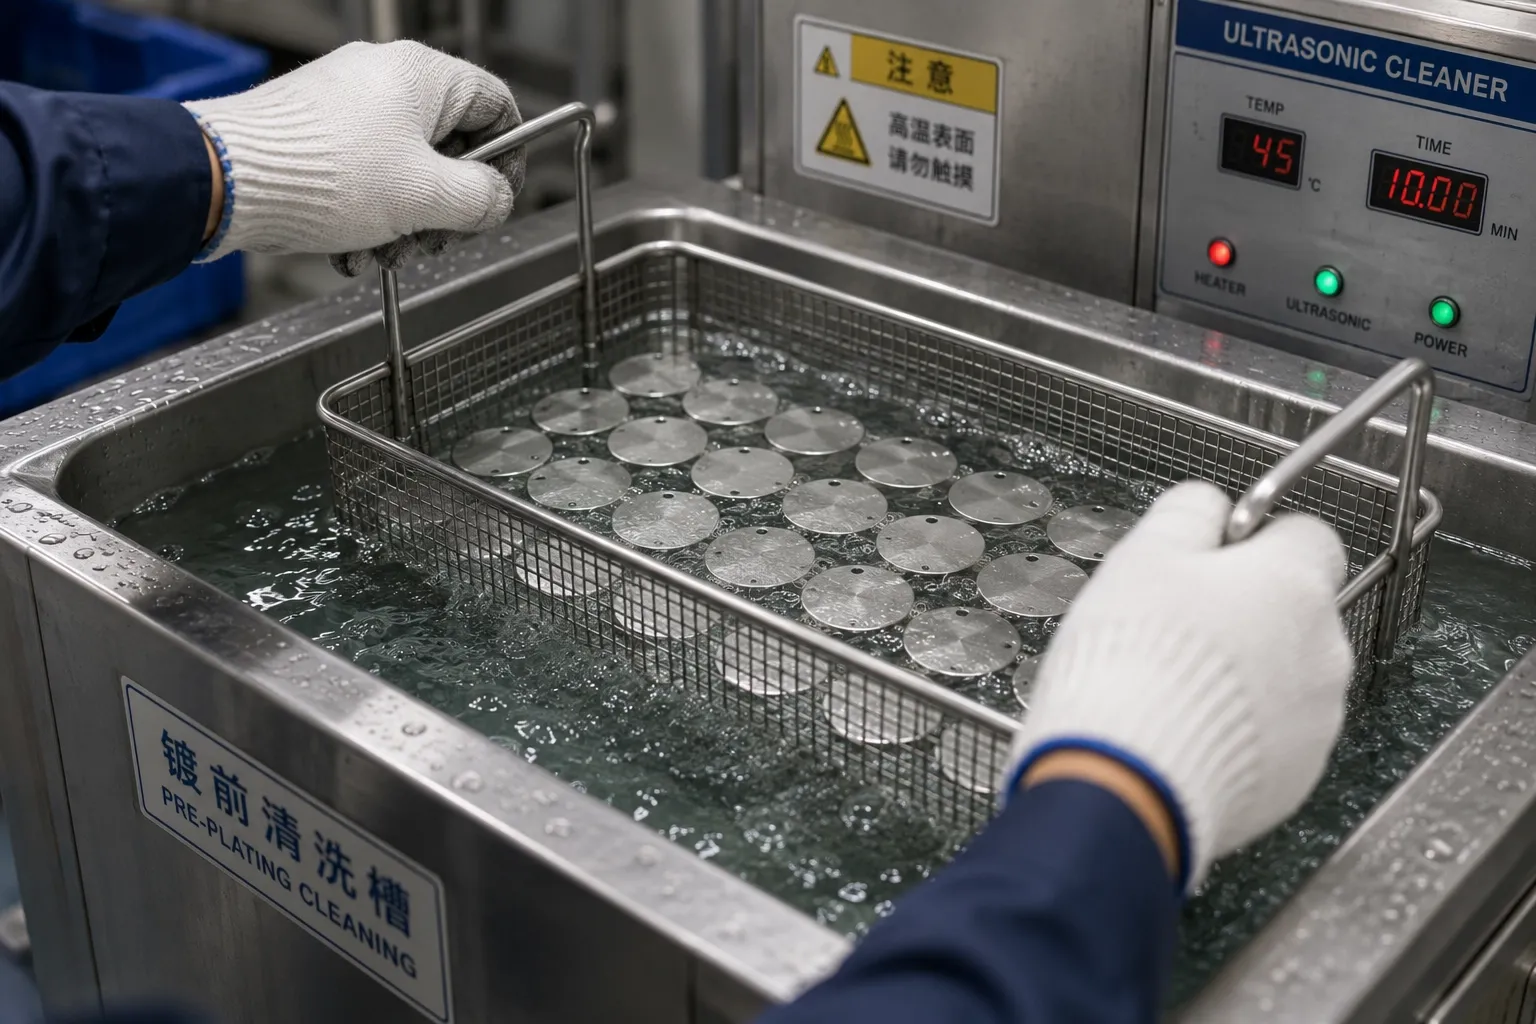
Cleaning before plating or coating
Process parameters
These are engineering properties of the process itself. They hold at any competent factory and can be checked against a manufacturing reference.
| Dimensional tolerance | ±0.05 mm |
|---|---|
| Minimum wall / section | 0.3 mm |
| Tooling cost | $150–2,000 (simple to progressive steel die) |
| Suited to | 1,000–500,000 pcs |
| Cycle time | Seconds per piece once running |
| Materials accepted | 316L stainless steel, Brass, Copper, Titanium |
Tooling ranges are industry-typical. A firm figure is quoted against your CAD file — see the cost breakdown.
Stamping vs Lost-wax casting
Choose stamping when the design is flat or shallow and the quantity justifies cutting a die; choose casting when the form is three-dimensional or has undercuts a die cannot release.
Compare with lost-wax casting →Materials and categories this suits
Process, material and product category are one decision seen from three sides. These are the combinations that actually work.
| 316L steel | ASTM A276 / EN 1.4404 |
|---|---|
| Titanium | ASTM B348 Gr.2 / Gr.5 (Ti-6Al-4V) |
| Brass | ASTM B36 / EN CW508L |
| Copper / bronze | ASTM B152 (Cu) / ASTM B505 (bronze) |
| Rings | Flat bands and blanks at volume |
|---|---|
| Necklaces & Pendants | Discs, bars, coin pendants, tags |
| Earrings | Flat studs, hoops and blanks |
| Bracelets & Bangles | Cuff blanks and link plates |
What to watch out for
Stamping and die striking — buyer questions
Each answer stands alone and can be read without the rest of this page.
What tolerance can stamping and die striking hold?
Stamping and die striking holds ±0.05 mm on production parts, with a minimum wall or section of 0.3 mm. Sheet or coil stock is blanked, formed and embossed between a matched pair of hardened steel dies under press tonnage. Tighter tolerances than this normally mean a secondary machining operation rather than a change to the primary process.
How much does tooling cost for stamping and die striking?
Tooling for this route is $150–2,000 (simple to progressive steel die), quoted as a one-off line and invoiced separately from the unit price. The buyer owns the tooling and it is not charged again on a reorder. Full tooling ranges for every route are on the manufacturing cost page.
What order quantity does stamping and die striking suit?
This route suits 1,000–500,000 pcs. Below that range the setup cost dominates the unit price; above it, a different route is usually cheaper per piece. Choose stamping when the design is flat or shallow and the quantity justifies cutting a die; choose casting when the form is three-dimensional or has undercuts a die cannot release.
Which metals can be processed this way?
316L stainless steel, Brass, Copper, Titanium. The die is the whole commitment. A design change after the die is cut usually means a new die, not a modification — so the CAD must be signed off before tooling starts. Undercuts and true three-dimensional forms cannot be stamped at all.
Stamping or lost-wax casting — which is right for my design?
Choose stamping when the design is flat or shallow and the quantity justifies cutting a die; choose casting when the form is three-dimensional or has undercuts a die cannot release.
Not answered here? All buyer questions →
Quote a stamping run
Send the CAD file or a sketch. You get the tooling cost as its own line, the unit price at your quantity, and a straight answer on whether stamping is the right route for the design — we will say so if it is not. Production runs in Qingxi, Dongguan, Guangdong.
- 01Reply within one working day, Guangdong business hours.
- 02Itemised cost sheet — mold quoted separately, not folded into the unit price.
- 03NDA on request before any file is shared.